3D Printed Rocket Parts: What Works & What Doesn’t
3D printing can produce useful model-rocket jigs and some flight components, but suitability depends on the particular design, material, print quality, heat exposure and launch configuration. The examples here are options to evaluate, not flight-test results from RocketMaterials. An Apogee printed-rocket case study documents printed airframe pieces and also deformation from hot ejection gases; a successful example does not qualify a different print.
Separate workshop tools from flight parts
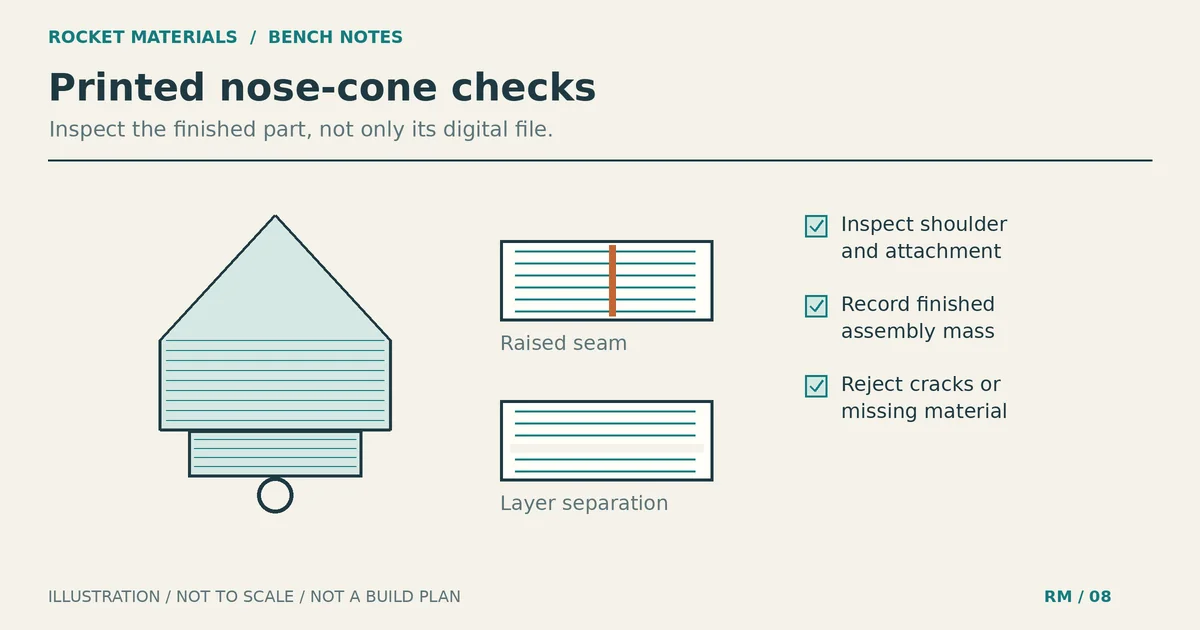
Fin-positioning jigs, marking templates and fit-check prototypes stay on the workbench, so they can be a useful way to develop a design. A printed nose cone, lug, fin can or tube becomes part of the flight vehicle: assess finished mass, balance/stability, print orientation, layer bonding, fasteners, retention, recovery loads and the actual operating environment. Weigh the finished component and measure its fit against the specific mating parts. Download popularity and a posted flight report are not qualifications for a new configuration.
Filament is not a flight rating
- PLA: straightforward for prototypes or jigs, but Prusa’s PLA guidance flags heat, UV and layer-strength limitations. A motor letter is not a service-temperature measurement.
- PETG: a printable option with different toughness and adhesion characteristics; Prusa’s PETG guidance describes printer-part applications, not protection from rocket ejection gas.
- ABS/ASA: assess the specific grade, printing requirements and exposure; neither material name proves an ejection shield.
- PA/nylon: grade, moisture conditioning and print settings matter; it is not an automatic heat-safety shortcut.
No universal wall thickness, infill, print orientation or tolerance certifies a flight part. Read the current supplier datasheet for the exact filament; nozzle and bed temperatures are manufacturing settings, not allowable service temperatures.
Heat and load-bearing parts
Do not replace manufacturer-specified recovery protection with an ordinary FDM parachute sleeve. For placement and material choices, see our recovery wadding guide. The NAR Model Rocket Safety Code calls for flame-resistant or fireproof recovery wadding, and Estes’ recovery-wadding explanation describes how hot ejection gases can melt a parachute. A motor adapter or mount bears load and may encounter heat: use a manufacturer-approved adapter or a validated design for the specific motor, case, retention and airframe. A fit check with a spent motor is not a loaded thermal or structural test. NAR specifies certified commercially made motors, not certified motor-mount substrates.
Printing is not categorically barred for high-power construction, but the NAR High Power Rocket Safety Code requires certification within scope and stability checks. Seek qualified design and range review for a high-power or modified structural print. Compare current purchase and print costs only with actual material use, failed-print allowance and a comparable commercial part.
One Comment
Comments are closed.